+86-18816569813
 EN
INVESTMENT CASTING / PROCESS SELECTION
A buyer comparing low-temperature and medium-temperature wax casting needs more than two melting-point figures. The useful question is whether the selected wax pattern, ceramic shell and finishing plan can produce the required industrial component from the actual drawing.
Short answer: Ask for a route-specific review of pattern stability, difficult features, the specified alloy, as-cast dimensions, machining and inspection. Choose after reviewing those answers and, where the risk justifies it, sample results. Neither label alone guarantees a tolerance or surface finish.
Three different temperatures: wax preparation and injection, ceramic-shell dewaxing or firing, and molten-metal pouring. A “low-temperature wax” route does not mean the finished metal part is intended for low-temperature service. The Investment Casting Institute's process overview shows how wax pattern production, shell building and dewaxing precede metal pouring.
FIRST DECISION
What Is Actually Different Between the Two Routes?
Both routes belong to the investment casting process family. Balasen lists low-temperature wax casting and medium-temperature wax casting as separate services. To compare them for one part, the supplier should describe the wax material and conditioning used on each proposed route, the pattern-making method and any changes to shell building or finishing. The route names do not, by themselves, provide that information.
PATTERN SYSTEM
What wax is used?
Request the proposed wax formulation or specification and the pattern-making conditions relevant to the job. Material behavior depends on more than a label.
PROCESS CONTROL
How is the pattern held to shape?
Compare injection, cooling, handling and assembly controls for ribs, long spans, thin edges and reference surfaces.
DELIVERED PART
What is finally inspected?
Ask which dimensions remain as cast, which faces are machined and how the specified material and inspection requirements are met.
The Investment Casting Institute's wax-room technical presentation explains why wax composition, melting, conditioning and injection influence pattern quality. It does not establish a universal accuracy ranking for Balasen's two named routes.
FOLLOW THE PART
Where Can a Wax-Route Choice Affect an Industrial Casting?
Think in stages rather than treating wax selection as a single number. The same drawing must survive pattern manufacture, shell preparation and metal solidification before its critical features can be checked.
DRAWING EXAMPLE / A
A Slender Bracket: Pattern Stability Comes First
Imagine a small industrial bracket with two mounting pads connected by a thin arm and several short ribs. The buyer needs the finished mounting points to line up; the connecting shape can remain as cast. This is an illustrative drawing scenario, not a documented Balasen production case.
Compare the two proposed patterns
Can each route fill the thin ribs without an incomplete pattern?
How are the arm and pads supported during cooling and assembly?
Which pattern dimensions will be checked before a ceramic shell is made?
Then check the metal drawing
Mark which pads require machining, the minimum wall or rib conditions, and the relationship between the finished mounting points. A stable wax pattern is valuable only if the cast metal and finished features meet this drawing.
DRAWING EXAMPLE / B
A Flow-Control Part: The Wax Name Is Only One Decision
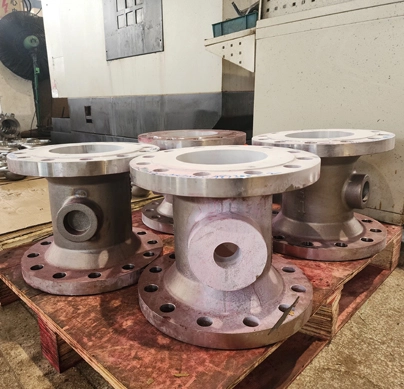
Now imagine a compact valve component with an internal opening, a mating flange and a sealing surface. Review how each route forms the opening and where a shell or core may be needed. Then mark the bore, flange and seal seat that must be inspected or machined.
If the finished bore or seal seat is the controlling feature, neither wax label alone answers the question. Compare the complete casting and machining plan, along with any material or leak-test requirement on the customer's drawing.
PROCUREMENT CHECKPOINT
Ask for Two Comparable Quotations, Not Two Generic Brochures
Send the same controlled drawing and requirements for both proposed wax routes. Request the following details side by side so an apparent price difference is not simply a different finishing or inspection scope.
If a general casting tolerance system is required, specify the applicable grade with the supplier rather than copying one advertised tolerance onto every feature. ISO 8062-3:2023 is an official reference for general casting tolerances and machining allowance grades.
THREE COMMON SHORTCUTS
What Should You Avoid Assuming?
Ask for the actual wax system, part geometry and measurable acceptance requirements. The result depends on the complete route.
Appearance does not establish bore fit, seal-face condition, threads or the location of a mating surface.
Confirm the critical dimensions, inspection condition and any separately machined features for the proposed part.
A SIMPLE SELECTION RULE
If only one proposed route can demonstrate the required pattern and finished-part results, choose that route. If both can meet the drawing, compare tooling, repeatability, total finishing scope, lead time and price. If neither can meet a critical feature, revise the design or evaluate another casting route before placing an order.
Low- and Medium-Temperature Wax Casting FAQ
Does “low-temperature wax” mean the metal part can operate at low temperatures?
No. Service-temperature suitability is determined by the specified metal material, processing and acceptance requirements, not the name of the wax pattern route.
Is one wax route always cheaper?
Compare the total quoted scope: pattern tooling, casting yield assumptions, machining, inspection, quantity and any first-article work. A wax name alone cannot establish the delivered-part cost.
What is the best information to send for route selection?
A current drawing or 3D model, material grade, estimated weight, annual and order quantities, marked critical features, finished surfaces and inspection requirements.
THE NEXT STEP IS A DRAWING REVIEW
Ask for the route that fits the part, not the route with the more attractive label.
Review Balasen's low-temperature wax and medium-temperature wax service pages, then send your drawing with the metal grade and finishing requirements for a part-specific proposal.